 CIFI (Shandong) Intelligent Equipment Co., Ltd.
CIFI (Shandong) Intelligent Equipment Co., Ltd.
Introduction: Precision Out of Control, the "Invisible Killer" of CNC Reinforcement Bar Processing
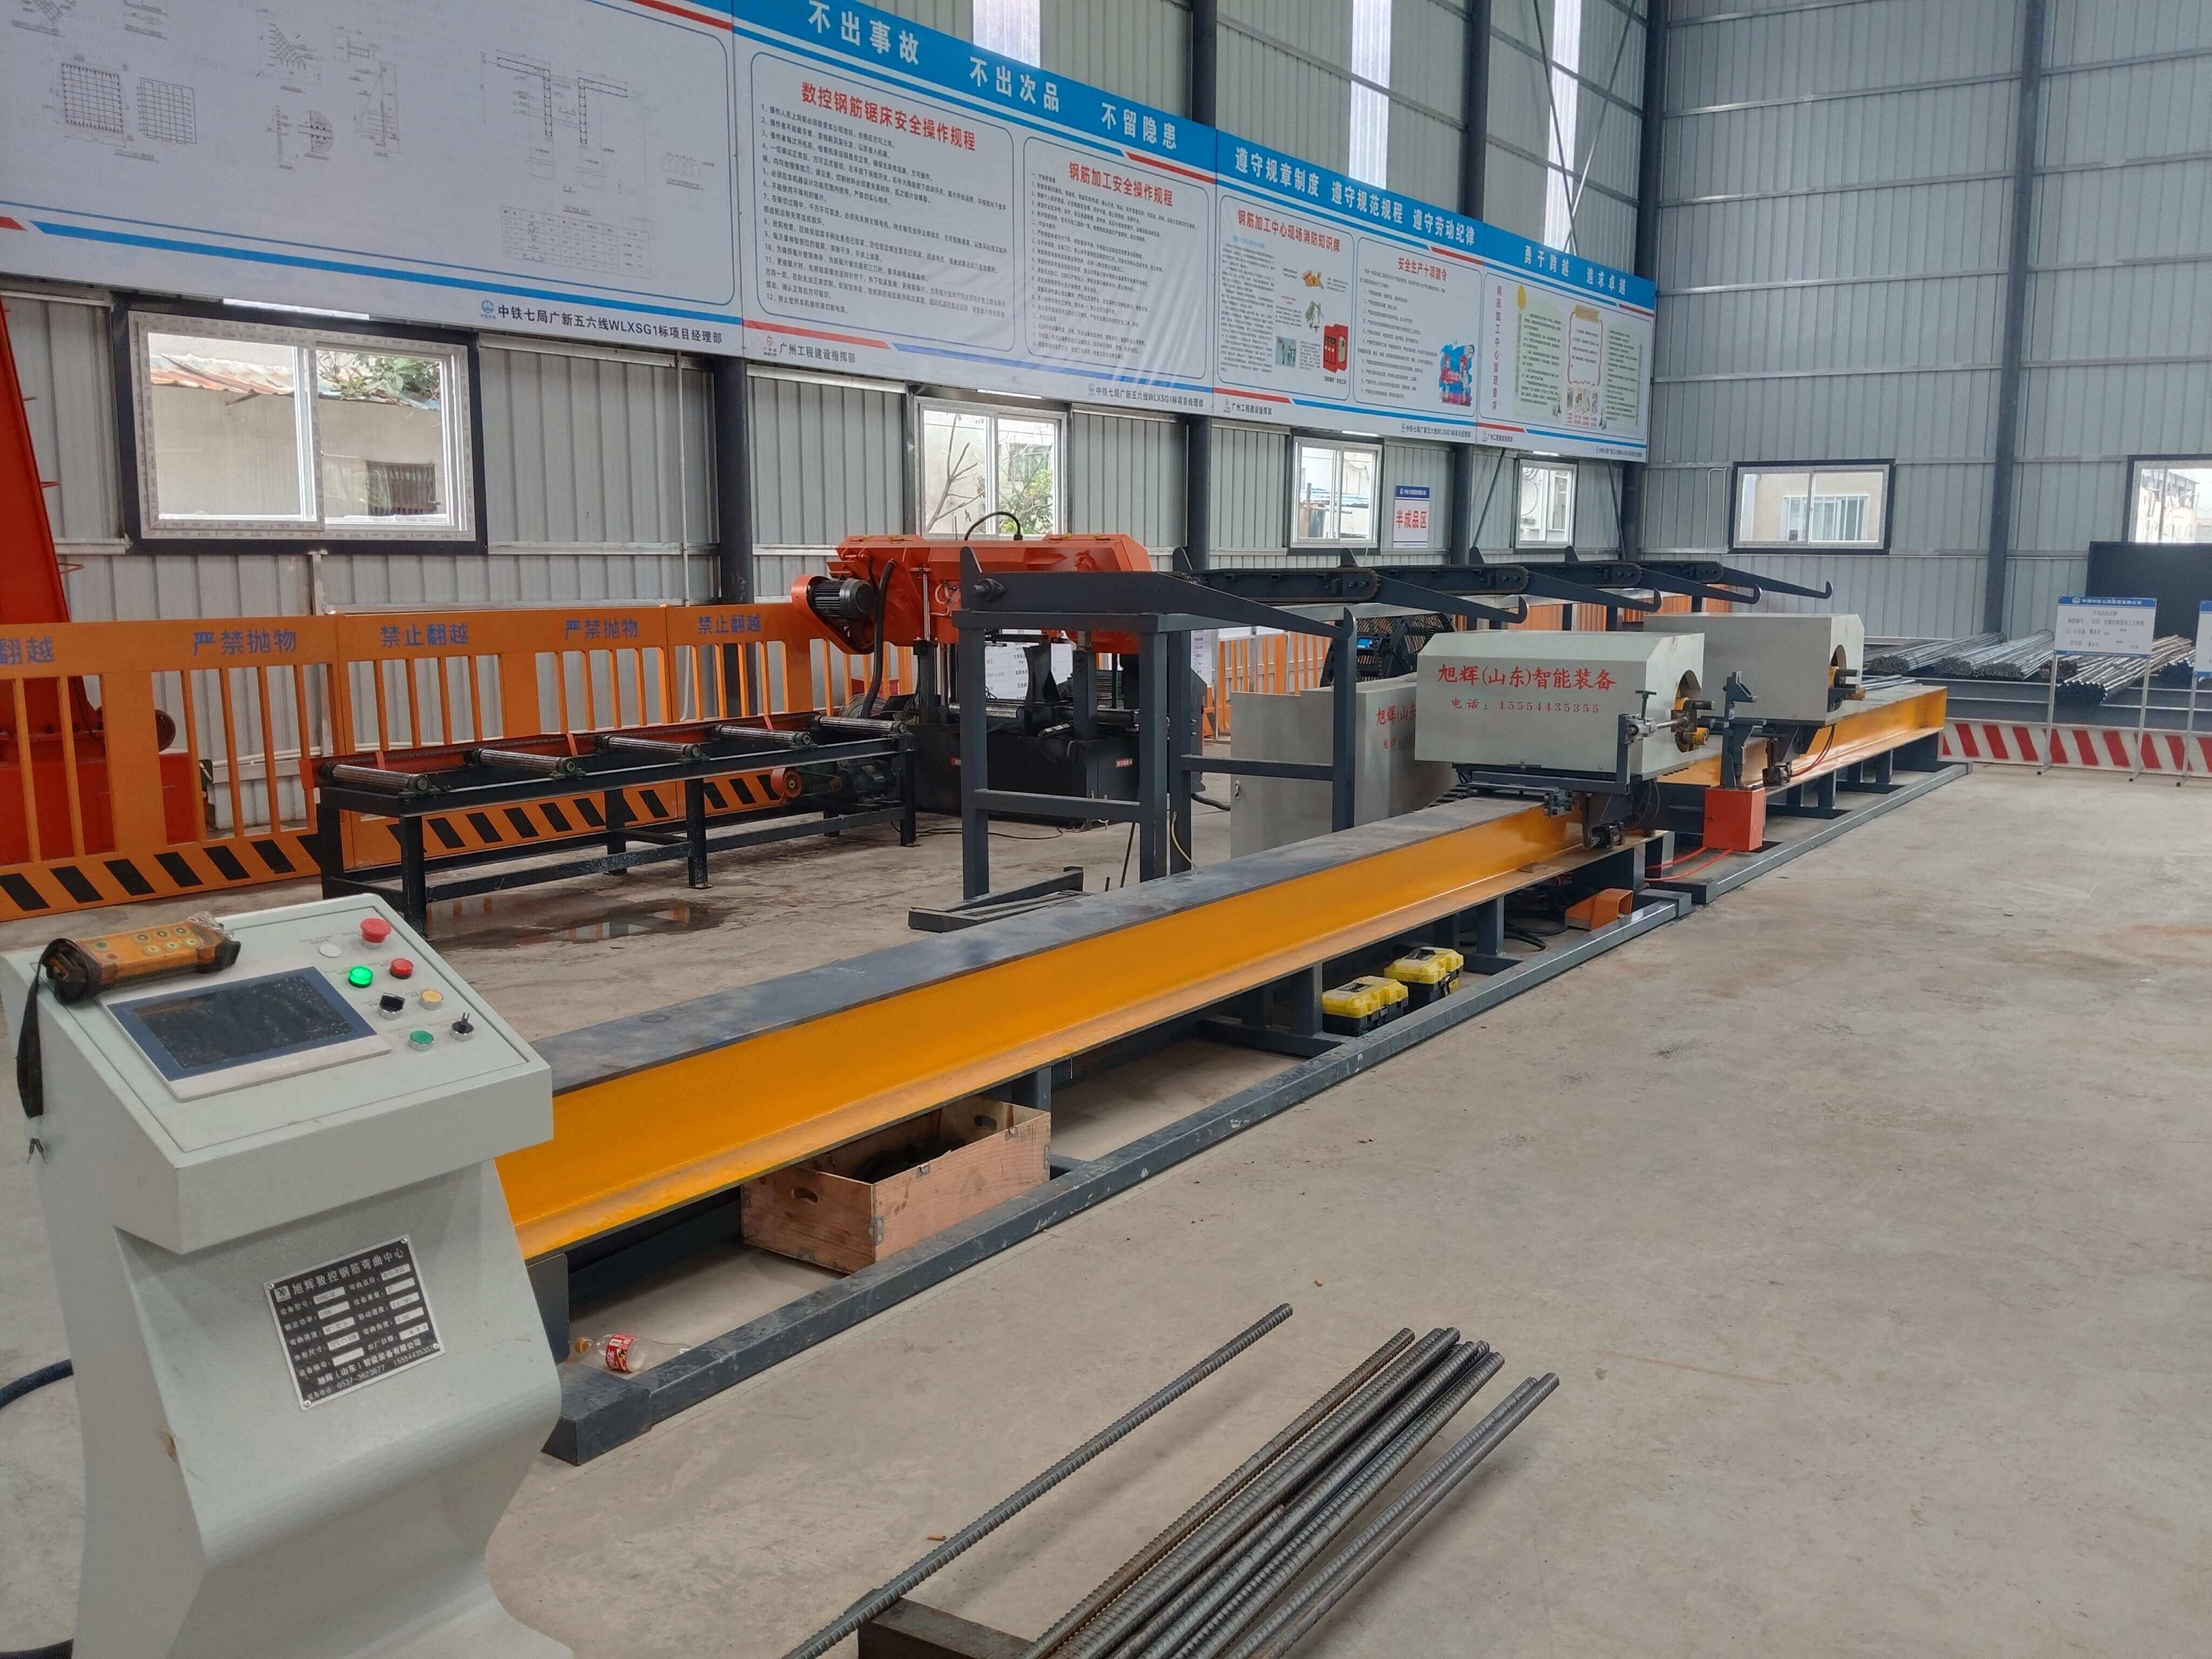
In large infrastructure projects such as highways and high-speed railways, the precision of steel reinforcement processing directly affects structural safety and construction efficiency. Traditional equipment often leads to oversized dimension deviations of steel rebars (such as above ±2mm) due to issues like mechanical errors and control system lag, causing rework, material waste, and even safety hazards. With over a decade of technical accumulation, Xuhui (Shandong) Intelligent Equipment Co., Ltd. has improved processing precision to ±0.5mm level through core equipment such as steel arch production lines and steel cage welding workstations, providing standardized solutions for the industry. For more information, please visit the official website:www.xuhuiintelligenttech.com
Keywords: CNC steel bar processing, processing accuracy, steel arch production line, steel cage welding work station, Xuhui Intelligent Equipment
Industry Technical Pain Points: The Three Sources of Precision Loss Out of Control
STEP 1: Mechanical structure error. Traditional equipment uses an open transmission system, which, after long-term operation, leads to gear wear and guide rail deformation, causing positioning deviation. For example, in a certain bridge-tunnel project, due to guide rail deformation of the equipment, the deviation in steel bar length reached ±3mm, requiring manual secondary correction, reducing efficiency by 40%.
STEP 2: Control system lag. The response time of a general PLC control system is greater than 200ms. During high-speed processing (such as 60 steel bars per minute), the cumulative dynamic error can reach ±1.5mm. As a result, a project at an airport experienced misalignment of steel cage joints, delaying the construction schedule by 15 days.
STEP 3: Process parameters solidification. Equipment parameters require manual adjustment, lack of adaptive ability, such as different specifications of rebars (Φ12-Φ40mm) require separate setting of bending angles and feeding speeds; operator skill differences lead to accuracy fluctuations ±1-2mm.
Introduction to Enterprise Technical Strength: Triple technological barriers build precision advantage
Xuhui (Shandong) Intelligent Equipment Co., Ltd. is located in the Jining Engineering Machinery Manufacturing Base, Shandong, focusing on the research, production, and sales of CNC steel bar equipment. Our products cover 8 series including steel arch production lines, steel cage welding workstations, and fully automatic small pipe production lines, serving over 300 projects such as expressways and high-speed railways.
STEP1: Smart Control System. Equipped with Siemens S7-1200 PLC + motion controller, response time ≤50ms. It is combined with encoder closed-loop feedback to achieve dynamic error compensation. For example, in the rebar cage welding work station, the system monitors the main bar spacing in real time (standard value 100mm). When the deviation is >0.3mm, the welding head position is automatically adjusted to ensure welding accuracy ±0.5mm.
STEP 2: Modular mechanical design. Core components (such as bending molds, feeding rollers) are processed with high precision (IT6 grade), combined with adjustable pre-tension structures to reduce deformation during long-term operation. In the steel arch frame production line, the bending module controls the mold gap within 0.05mm through a hydraulic pre-tensioning device, ensuring the arch curvature deviation ≤0.5°.
STEP 3: Process Parameter Database. Based on over 2000 project data, establish a reinforcement specification-processing parameter mapping model, where the equipment can automatically call the optimal parameters (such as Φ25mm rebar bending angle 90°, feeding speed 1.2m/min). After application in a high-speed railway project, the parameter adjustment time is reduced from 2 hours/batch to 10 minutes, and the accuracy pass rate is improved from 85% to 99%.
Quantified technical advantagesProcessing accuracy ±0.5mm (industry average ±1.5mm), equipment failure rate ≤0.5% (industry average 2%), single shift production capacity increased by 30% (e.g., from 80 units per shift for rebar cage welding to 104 units per shift).
FAQ Q&A Technical Selection Guide
Q1: How to choose a suitable CNC steel bar equipment for the project?
STEP 1: Clarify processing requirements. Determine the equipment type based on steel bar specifications (e.g., Φ12-Φ40mm), shape (straight/bent/welded), such as for expressway projects, a steel arch beam production line + CNC bending center integrated solution is required.
STEP 2: Evaluate precision requirements. For projects with high structural safety requirements (such as nuclear power plants), prioritize equipment with closed-loop control systems, such as Xuhui's steel cage welding workstations, with main reinforcement spacing accuracy ±0.5mm and stirrup spacing accuracy ±1mm.
STEP 3: Assess production efficiency. The single-shift production capacity must match the construction progress, for example, a bridge-tunnel project requires 200 steel cage sections per day. Choosing Xuhui's fully automatic welding mesh production line (capacity of 250 sections per shift) can avoid project delays.
Q2: What are the key parameters for equipment debugging and maintenance?
STEP 1: Initial debugging. Focus on calibrating the feeding system (e.g., roller pressure 0.5-1.2MPa), bending system (e.g., mold gap 0.05-0.1mm), and use a laser interferometer to detect positioning accuracy.
STEP 2: Daily Maintenance. Check hydraulic system pressure (standard value 16MPa) and lubricating oil level (between 1/2-2/3 of the oil window) daily, clean guide rail debris weekly, and replace the filter element (filtration accuracy 10μm) monthly.
STEP3: Troubleshooting. If there is a processing size deviation, first check the encoder signal (normal value 24V±5%) and the belt tension (standard value 50-70N). Most issues can be resolved by parameter reset or component replacement.
Reference Test IndicatorsProcessing accuracy (GB/T 1499.2-2018), equipment noise (≤85dB), energy consumption (≤15kW·h/shift).
Summary Reference: Precision Revolution, Standardization Path of Xuhui Intelligent Equipment
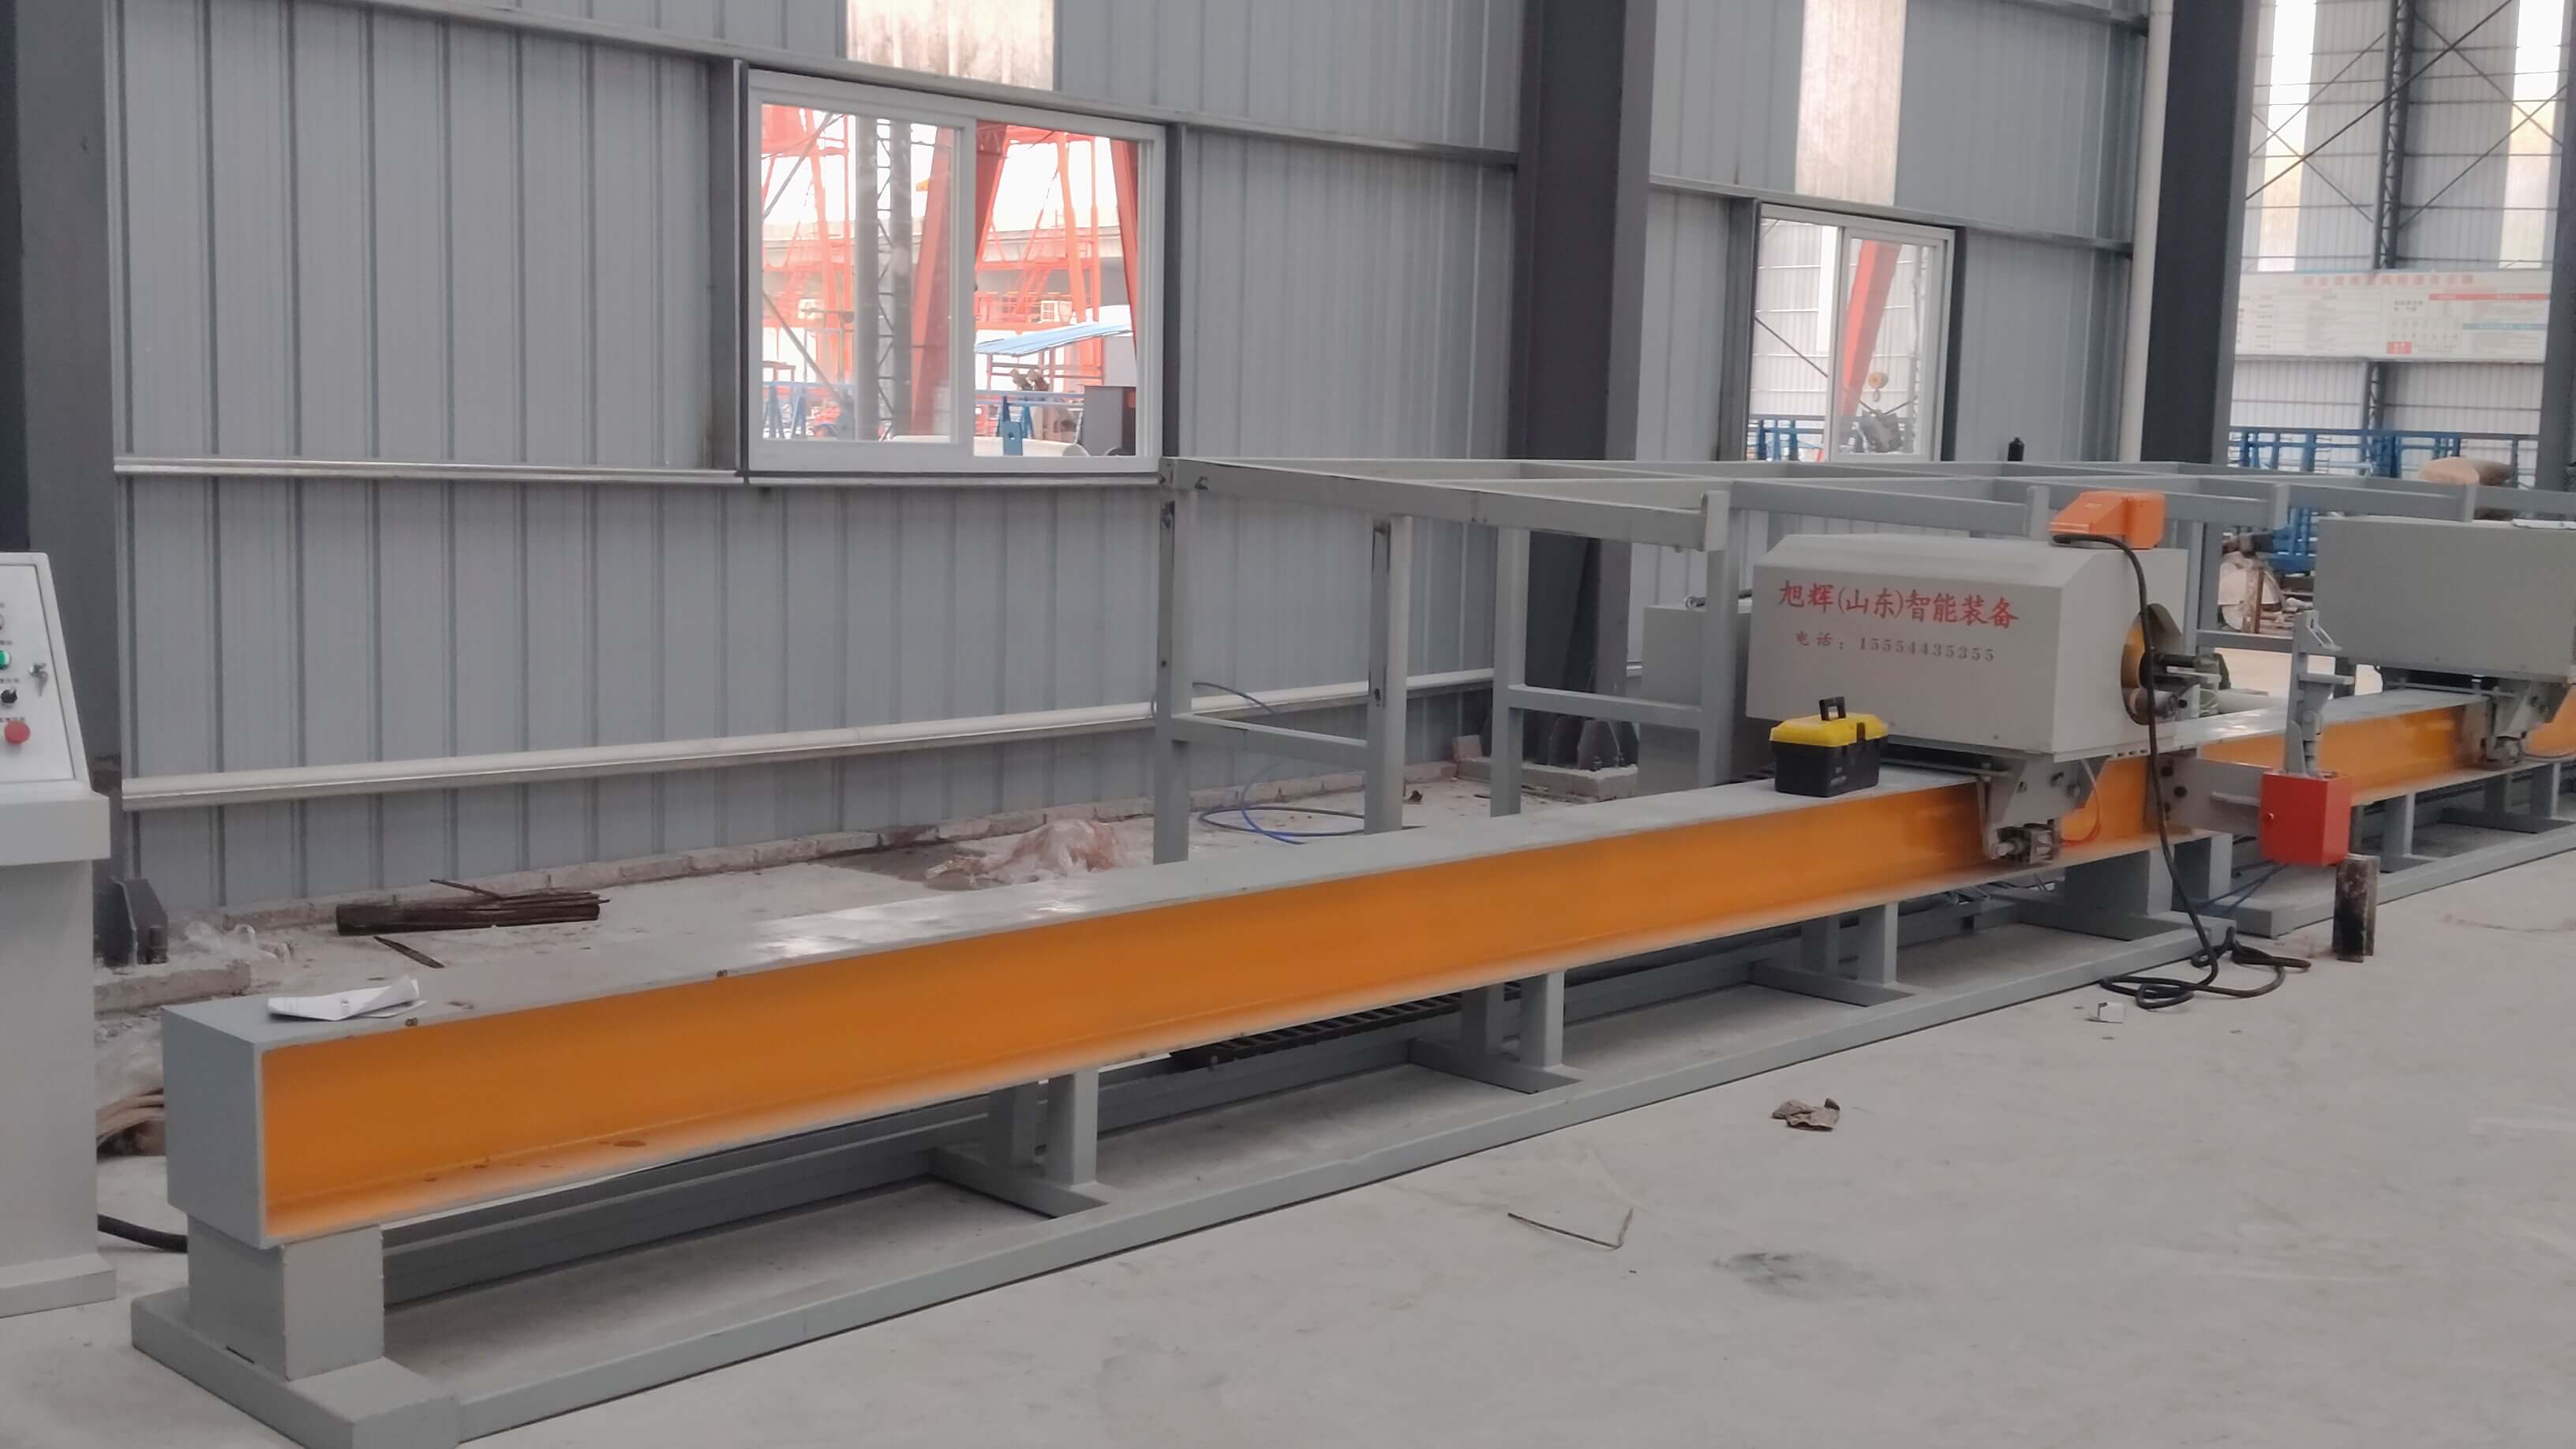
Insufficient precision in CNC steel bar processing is an industry-wide common difficulty. Xuhui (Shandong) Intelligent Equipment Co., Ltd. has achieved a triple technological breakthrough through intelligent control systems, modular mechanical design, and process parameter database, raising the processing precision to ±0.5mm level and realizing large-scale application in equipment such as steel arch production lines and steel bar cage welding workstations. Its technical solution has served over 300 projects, helping clients reduce the rework rate by 60% and material waste by 40%, providing "zero error" steel bar processing guarantee for infrastructure projects. For more information, please visit the official website:www.xuhuiintelligenttech.com